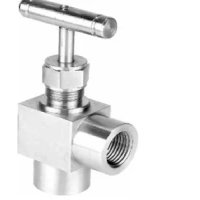
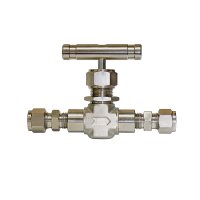
Instrumentation needle valves across 120 listed configurations — straight and angle pattern, DN6 to DN25, rated 6000 to 10000 psi, in SS316, SS304 and brass bar stock.
Sourcing at a Glance
- HS Code(s)
- 8481.80 (six-digit; 8-digit ITC-HS pending CHA confirmation)
- MOQ Range
- Quoted per order
- Sample Lead Time
- Quoted per order
- Production Lead Time
- Quoted per order
- FOB Basis
- Quoted per order
- Standards / Certifications
- MSS SP-99, ASME B1.20.1
Specifying Needle Valves: Pattern, Pressure Class and Body Material
Fine control, not flow capacity. A needle valve's tapered stem closes gradually into a small conical orifice, giving a degree of flow-rate resolution that a ball or gate valve — designed to open a full bore quickly — cannot match. That is the entire reason the family exists: instrument bleed lines, sample points, gauge isolation and calibration duty need precise, repeatable small-flow control far more than they need throughput.
Pattern. Straight pattern keeps the flow path in line, the default absent a specific layout constraint. Angle pattern turns the outlet 90°, which is common wherever panel or manifold space is tight and a straight run would require an extra elbow fitting.
Size and pressure. DN6 to DN25 (⅛" to 1") across 120 configurations, at 6000 or 10000 psi. This is the second-smallest catalogue in the entire valves category — only Instrument Manifolds (96 SKUs) is smaller — needle valves occupy a genuinely narrow product envelope, yet independent market reference material for this category is unusually extensive relative to its catalogue size — outside documentation exceeds what's in Himalay's own 120-SKU listing.
Why the pressure ratings run so high at such small bore. Instrument and sampling lines commonly tap directly off high-pressure hydraulic, gas-sampling or well-testing systems, and at DN6–DN25 a solid bar-stock body can economically hold 6000–10000 psi in a way a cast body of the same bore could not. This is also why needle-valve bodies are machined from bar stock rather than cast — bar stock is generally favoured over casting at this bore-to-pressure ratio to minimise porosity risk.
Materials. SS316 bar stock is the general instrumentation standard, giving corrosion resistance across most process media. SS304 serves less aggressive service at lower cost. Brass suits air, water and non-corrosive utility instrumentation where the cost saving matters and the medium allows it. Trim is an integral hardened stem tip on all listed configurations — the tip itself is the sealing element, machined into the stem rather than fitted as a separate part, which is what gives the fine, repeatable seating this family is specified for.
Standards. MSS SP-99 governs instrument valves — needle, packless, ball, plug, check and manifold types — for steel and alloy construction at NPS 2 and below, rated to 15,000 psi at 100°F. ASME B1.20.1 governs the NPT thread form on threaded-end valves.
Conformity. CE for the EU, SABER for Saudi Arabia, ECAS for the UAE, EN 10204 3.1 certificates as the EU procurement baseline.
From spec to RFQ. State the tap-off system pressure, medium, required flow-control resolution, connection type, body pattern and material, and destination market. Share the instrument line list with your RFQ and the valve is matched against the catalogue directly.
How Needle Valves Work
Mechanism: a tapered plunger closing gradually into a matched conical seat. "A needle valve has a relatively small orifice with a long, tapered seat, and a needle-shaped plunger on the end of a screw, which exactly fits the seat." Turning the screw retracts or advances that plunger, and "as the screw is turned and the plunger retracted, flow between the seat and the plunger is possible; however, until the plunger is completely retracted, the fluid flow is significantly impeded" — the seal only fully releases at the very end of the stroke. The fine-threaded screw is what gives the valve its resolution: "since it takes many turns of the fine-threaded screw to retract the plunger, precise regulation of the flow rate is easily possible" — a geometry a quarter-turn ball valve or a shorter-travel globe valve cannot reproduce at the same bore.
Industries served: protecting instruments from surge, and metering flow too small for a general-purpose valve. "All field analog instruments are fitted with a needle valve to control flow entry, where sudden surges of fluid under pressure can damage the instruments" — the valve's job on an instrument line is as much protective as it is about flow-setting. The same fine-throttling geometry is specified "in all industries for controlling and metering fluid applications such as steam, air, gas, oil, water, or other non-viscous liquids," and at sample points in piping "where the flow must stop gradually and... precise adjustments of flow are required." Outside process plant, the same geometry shows up wherever a small, steady flow has to be dialled in and held — Wikipedia cites "vacuum systems, when a precise control of gas flow is required, at low pressure, such as when filling gas-filled vacuum tubes, gas lasers," and pressure-gauge shutoff duty. That range, instrument protection at one end and precision metering at the other, is consistent with Himalay's own catalogue sitting almost entirely in threaded, bar-stock, high-pressure configurations rather than larger flanged process sizes.
Standards landscape: an instrument-valve design standard, plus the thread standard that governs how it connects. MSS SP-99 governs instrument valves — needle, packless, ball, plug, check and manifold types — for steel and alloy construction at NPS 2 and below, rated to 15,000 psi at 100°F. ASME B1.20.1 sits alongside it for the threaded-end connections: it is "the foundational Standard for NPT, NPSC, NPSM, and NPSL pipe threads," covering "dimensions and gaging of the world's most common pipe threads," used, in ASME's own framing, in everything "from critical applications demanding robustness and precision to common plumbing and hardware." On a needle valve, thread dimension and gaging matter directly: a threaded NPT connection is a tapered, sealant-dependent joint rather than a parallel thread, so gaging tolerance affects whether the joint holds at the pressures this family is rated to. Sources: [Wikipedia — Needle valve](https://en.wikipedia.org/wiki/Needle_valve); [Hardhat Engineer — Needle Valve: A Complete Guide for Engineer](https://hardhatengineer.com/needle-valve/); [ASME — B1.20.1 Pipe Threads, General Purpose, Inch](https://www.asme.org/codes-standards/find-codes-standards/b1201-pipe-threads-general-purpose-inch)
Frequently Asked Questions
- Straight or angle pattern — which needle valve should I specify?
- Straight pattern keeps inlet and outlet in line — the default where panel layout is unconstrained. Angle pattern turns the outlet 90° from the inlet, which saves space and simplifies tubing runs on crowded instrument panels and manifolds, at the cost of a slightly more complex flow path. Both are listed. State your panel or manifold layout constraints.
- Why use a needle valve instead of a ball or globe valve on an instrument line?
- Because the tapered stem-into-orifice geometry gives fine, repeatable control over very small flow rates — well suited to instrument bleed, sampling, calibration and gauge-isolation duty, at a resolution a ball or globe valve, designed for larger flow, is not built to match. Needle valves are also compact and rated to very high pressure relative to their size, matching typical instrument-line duty. State the flow rate you need to control, not just the line size — needle valves are chosen for control resolution, not throughput.
- Why are these valves rated to 6000 or 10000 psi at such small sizes?
- Because instrument and sampling lines routinely tap directly off high-pressure process lines — hydraulic systems, high-pressure gas sampling, well-testing manifolds — at a bore small enough (DN6–DN25) that a bar-stock machined body can economically hold that pressure. State the actual system pressure the valve will tap into, since needle valves at this scale are rated well beyond typical process-line classes.
- What conformity documentation applies for EU, Saudi and UAE imports?
- CE marking for EU-bound equipment per applicable directives, SABER for Saudi Arabia, ECAS for the UAE, with EN 10204 3.1 material certificates as the EU procurement baseline. State the destination market in the enquiry.
Last verified: 6 August 2026
Request a Quote for Needle Valves


